Welding Cast Iron

Put the piece that you want to weld in regular sand. Use a cast iron nickel rod. Weld at the lowest temp that you can get. When you weld, only go an inch at a time and let it cool or it will spidercrack. Not as hard as you think.
 
If its cast steel you can weld it with MIG or 7018 or even 6011.If its cast iron your only choice is Nickel or some way with a torch,or a blacksmith or something.Most stuff is cast steel nowdays.Heat it up a little,like enough to burn the oil and grease off of it but no where close to red hot,weld an inch at a time and clean the slag real well,even grind it before the next weld,and dont stop until you are finished.If its a long weld you might heat it up again as you are welding to prevent a crack.If it does crack,fix it right then.Also you should grind a vee in the pieces if they are very thick.
Im just waiting for the attack now.But I doubt if its cast iron.If its cheap cast steel it will probably crack again.There is also a way with a torch and some kind of high dollar rods.Nickel rod is a waste of time most of the time.It is too brittle,costs a lot and if it breaks again you have to grind it all off and weld it with something else.
 

Trucker,

Your crainial rectal inversion is showing
again, did we not go thru this cast iron --
cast steel discussion last summer ?

Get the bare cast iron rod ,the flux and go
at it with a torch,rest assured it's cast iron.

george
 
To determine whether it is cast steel or cast iron hold it to a grinding wheel. Cast iron produces Red sparks and cast steel produces White sparks.
 
Gary, I'm no welding expert, as someone will no doubt proclaim, but I've had success using stainless steel rods for repairing broken cast iron parts. I guess they contain some % of nickel in their makeup. I weld about an inch, peck on it with a chip hammer until I can lay my hand on it, weld another inch and so on. . .

There's surely not much stress on a BBQ burner, but I guess something caused it to break. . .

Just an idea that has worked for me. . .
Paul
 
It would be one expensive BBQ to be made out of cast steel. It would be some kind of really, really poor cast steel to break! Being that it's a BBQ, arc welding it with nickel rods should be fine with some preheat.
 
It broke when I dropped it from about waste high. I would just replace but these things run about $40.00 each. So I thought I might just see if I could weld it back together.
 
I have had luck with UTP Econocast rods. Airgas carries them. Have repaired sprockets, brackets, collars, and more with them. Good luck!
 
I knew it! You all always do the same thing. You dont find a lot of stuff made with cast IRON. This might be,but not a lot of stuff. Basically all of the stuff that you all claim is cast iron is actually cast steel.
I have argued with you all until I just quit,but I didnt find anywhere that there were any tractor parts that were what you can call cast iron any more,its all cast steel.At least American made stuff.Of course you can weld it with a torch and the high dollar cast rods they have,I forgot what they called them on the muggy weld website,and probably other stuff as well.
Where the problem is that you all seem to think this stuff is cast iron and its not.Just because somebody said cast iron,doesnt make it cast iron.Plus after looking and looking myself,I didnt find where a bunch of stuff is made with cast iron.
Before you go jumping on me again about this stuff you all need to read a whole lot more about it.The way stuff is recycled and all there is not very much cast iron.There are different grades of cast steel.LIke cheap China junk is not close to as strong as American or anywhere else made steel for that matter.
Plus,in the past when we have done this,somebody will say that some part is cast iron,and its obvious its cast steel,but of course the "expert"has to know its cast iron because he said so.Well no he probably doesnt know,and calls cast steel cast iron because somebody told him it was cast iron and they were wrong.
I did find where engine blocks had more iron to them than other cast parts,but you can still weld them.
There were pictures of sparks and all kinds of stuff,and great long arguments,and other pictures and all kinds of things,but once it was all over,there was still very little cast iron.Cast Iron was way back in the days of steam engines and other stuff.In fact the furnaces that they built here were for steel.They had cast steel in the USA way back.Now they had iron too,but they made a lot of steel.
They still have cast iron.But there is way,way,way,more cast steel.
Argue all you want.There are also other types of steel called ductile,but once you see it you can spot it real easy.
This burner could actually be cast iron,but what do you want to bet its not?If you can weld it,its cast steel.
 
Well, Jo had part of it right...the cast iron will give off orange sparks on a grinding wheel. Also, if you try to drill it, it will have crumbly shavings. When you take a cape type chisel to vee the crack out, it will not curl a shaving, they will break off. Makes no difference if it is cast iron or malleable iron which is cast that is heat treated for about a week at a high temperature which gives it just a touch of bending before it breaks. You can identify it by a wider edge than just sand cast. Any other fire box quality steel would be CMO which would be carbon molybdenum steel. You would call it something like 4140 steel. The old rule about welding cast is...any electric rod with nickel in it. Seems the more nickel in it, the less apt to crack...but to be safer, weld only 3/4" at a time and use a small ball peen hammer and hit it just hard enough to make indentations in the bead. This helps to relieve any stresses set up in the last weld bead while it is still hot. If a crack is very long, like in a motor block and 6 or 8 inches long, I will vee two or three places perpendicular to the crack an inch or so long and weld them first to keep the crack from shifting and cracking more. Chasing a crack is not a money maker for who ever is paying the bill. Also, any little pin holes in the bead are caused by oil or contaminants down in the crack. They should be ground out and rewelded. Sometimes, if the job permits, you can heat the cast red hot before welding to burn out those things that make the little pin holes. This is my story and I think most of the welders who have welded cast iron for a living will pretty much agree with these methods. One other thing...the old John Deere cast iron with a lot of black carbon when you go to veeing it out does not weld hardly at all for me. Thats all. ohfred
 
Alright,I posted some again from what I was able to look up.I didnt want to mess up this post,so the info is on the post I made for steel.
Basically what I found was that you cant weld white cast iron,which is used in railroad wheels,plowshares and dies.You probably can weld gray cast iron as its almost sure to be some mixture rather than the same carbon content as other cast iron.I dont know where the carbon content is for when it wont weld,but there are different grades of cast iron the cheapest being less weldable.
Now you can say whatever you want and you may have a lot of experience messing with it where I dont,but I do know that welding stuff with nickel rod that doesnt need to be is a real problem when somebody has to fix it with a welding rod.I also nearly forgot,but there are better choices of welding rod than nickel,but they are expensive.I dont remember what these welding rods are called,except super rod,but they do work on cast steel very well.So does 7018 and even 6011 and MIG.
Not in the story I posted,but somewhere else I read that Gray cast Iron is considered cast steel.I dont know whether or not thats true,but it does say it can probably be welded.That would mean it has to be a mixture that is weldable,whether you call it iron or steel.
Now what were you saying about a cranial inversion? Ive done my homework,although I doubt that you will see it that way.I cant change your mind for you.If you dont want to believe me,I cant stop that.However maybe you can try with an arc welder before you say Im wrong at least.You could be surprised.
Also the story about steel is interesting no matter what you think.Carnegie built a Bessemer furnace in 1855.That was to make steel,not iron.Which is why we have so much steel now.Also everything is recycled nowdays.So because it has to be hard is why they use white iron,I guess it costs more or something because of the mixture and whatever else they do to it,the other stuff is a different mix.
 
Go to a welding supply or specialty rod supplier and they will have the proper rods to weld it with along with the correct procedure, ie. preheat temperature, peening, etc. It will probably say on the package as well. A specialty rod supplier might just give you a couple rods to try out. You can be rest assured that it is cast iron though. Cast iron doesn't distort as much with heating and cooling cycles. That's a big reason why it's the material of choice for engine blocks.
 
I’m so glad I saved this, saves a lot of typing


Most of this was taken right out of Lincoln’s book “Metals and How to Weld Them.”

First off there are six different types of cast iron so you need to know the type of cast iron you are dealing with. Manifolds and cylinder heads are Gray cast iron. If preheating can be used, the preheat temperature for shielded arc welding (stick) should be held between 500° and 1200°. When oxyacetylene welding you should preheat between 900° and 1200°. You should never let the object being repaired get over 1450°. Make your repairs, then place the object in your kitchen oven, (if it will fit) at 500° for 24-hours. I would purchase the proper temp sticks from your local welding supply.

Nickel 99 can be cut, drilled, milled, and ground. Ni-55 can be ground. The low nickel rod can't be even ground.


Other suggestions:

Ni-44 for Tig rod

Certanium 889, (stick)

Crown Alloys 255 (stick)

Lincoln Softweld 55 (stick)

Harris / Welco 65 (stick)

Ni-55 (stick)
 
I saved this from another site.

I do a lot of cast iron repairs with 100% success so far. Last year, after several months of research, I found information on a couple websites & mostly in an old Lincoln Welding book. The process is called "Cold Welding Cast Iron With MIG". I practiced several weeks on broken cast iron parts & broken/cracked manifolds my bro' gave me to get my technique down pat. It has worked with superb results.

I use MIG, 309/309L .030 wire, 98/2(AR/CO2) @15cfh & generally in the 80A range. You can use any gas with a mix of no more than 5% CO2 (ex:95/5). The 309 wire has a carbon content of .01 & works best. The idea is to keep the temperature cool by running short beads <1" & allowing the joint to cool before continuing. After running the short bead, you can take your glove off & lay your hand on the metal & will feel only warm to the touch. Since your pieces are not large, I would suggest shorter 1/2" beads & allow each weld to cool back to room temp before continuing.


Gary,

The local pizza shop brings me the burners
out of their ovens to weld as I am the only
shop in the territory that welds with O/A .
Welded with O/A they don't break again in the
same place .

For you guys that always want to use arc
weld of any kind ,try this with an arc.

The rest of the sequence is at the link.

george

<p align="center">
manifold03-2.jpg


Showing back of the broken heater box</p>

<p align="center">
manifold27.jpg


assembled box , back side</p>
rest of sequence
 
(quoted from post at 13:17:40 06/28/11) Basically what I found was that you cant weld white cast iron,which is used in railroad wheels,plowshares and dies. quote]


The part about railroad wheels being white cast iron is incorrect.

All cast iron railroad wheels that were still around by the late 1960's were mandated to be changed out per AAR Rules and FRA (federal law).
Cast iron rr wheels have been extinct now, for more than 40 years. :shock:
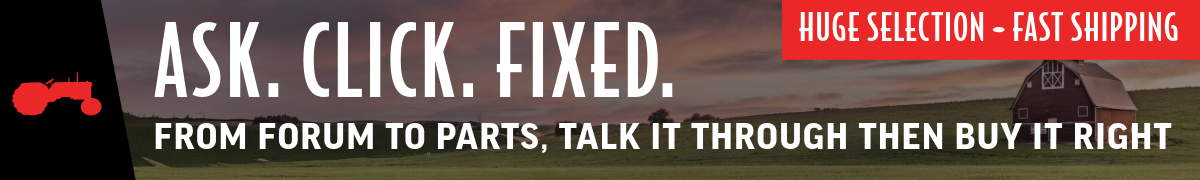
 
Nice job, cast iron rod and flux is the only way to have done that job. It is good to see some one with some practical experience in O/A welding post this. The man that taught me to weld was active as a welder for 60 years on everything from heavy equiptment to natural gas pipelines. He did a very similar repair to the cast iron manafold of an international O6 tractor I wish we had of done a before and after pic like you did. The manifold started out with about a 3"x3" chunk missing out of it and he just rebuilt it with cast iron rod and a O/A torch. But I guess comapred to an expert like trucker 40 even a man with that much knowledge and experince wouldn't know anything. It is a shame that some of these people think that they can read an article on the net and know every thing there is about the subject. I was fortunate that I was able to learn from his accumulated knowledge.
 
I completely agree with George about welding cast with the oxy-acetylene. My torch skills were never worth bragging about. I saw a fellow weld a small casting with the torch at a Henrob 2000 demonstration. I have since repaired 4 castings with the torch with complete success. May not be the best looking welds but they do hold.


Puddles,

I thank you and broken gun for the
compliments , not every one understands what
is involved in cast repair. I am not a good
welder but I get by,several of my customers
are really good welders (stick) and when I
need a piece done with no inclusions I get
one of them to weld it. I do the cast iron
and other things like spray weld and metal
spray , 1/2 or more of the work comes from
other shops.
Most of the manifolds are for antiques or
show pieces , so they need to be nicely
done.

george
 
A discarded gas barbeque grill would make a good preheat and slow cool down rig for cast iron welding.Most grills can be repaired,new stainless burners dont cost that much.I have some info some where a fellow welded an exhaust manifold for his daughters car using a grill.Stealer wanted 360 bucks for a new part.I just destroyed 6 special bolts holding my trucks pickup bed on to the chassis.I hear the stealer gets 20 bucks each for these bolts.I buy hex bolts for 1.50 a pound so it look like Ill be using hex bolts and flat washers to put it back together.
 
Yesterday's Tractor Forums

We sell tractor parts! We have the parts you need to repair your tractor - the right parts. Our low prices and years of research make us your best choice when you need parts. Shop Online Today.

Back
Top